
Flexible PCB Assembly

OrinewPCB · One-stop specialized PCBA
Flexible PCB assembly from released flex data to tested boards
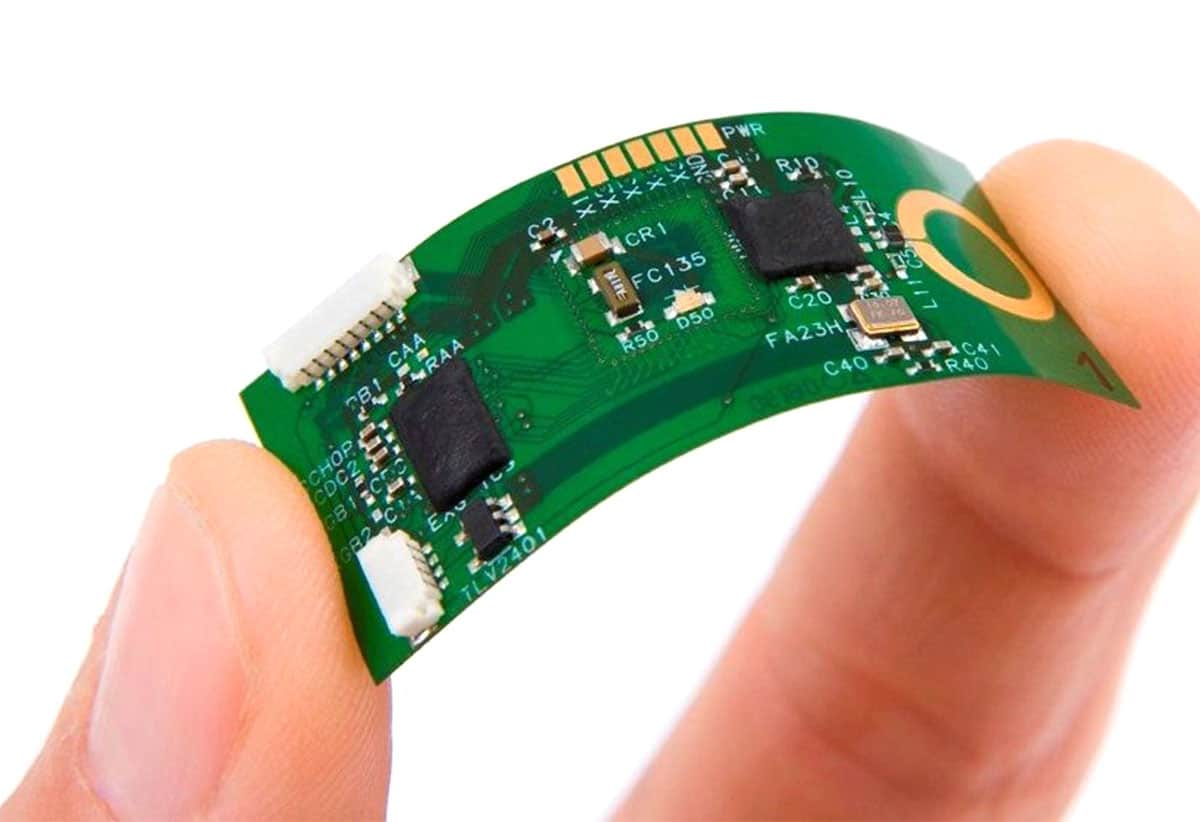
Flexible PCB assembly mounts and solders components onto a flexible circuit while controlling support, handling, thermal exposure and bend-area risk. OrinewPCB coordinates flex fabrication, 100% new original component sourcing, SMT/THT operations and agreed testing for prototypes, high-mix programs and low- to medium-volume orders.
The assembly plan should treat the flex construction and the fitted components as one system. Stiffeners, unsupported areas, panel or carrier design, connector alignment and the intended bend condition can affect printing, placement, reflow, inspection and final handling. We review these items before confirming price and the earliest practical delivery.
High-mix, practical quantities
OrinewPCB coordinates prototypes and low- to medium-volume builds, including several board variants, without losing revision and material ownership.
100% new, original parts
For components sourced by OrinewPCB, the requirement is 100% new and original. Manufacturer and distributor cooperation supports price, availability and lead-time review.
Quality and delivery together
The nine-step workflow remains in the plan while engineering and purchasing work toward the earliest practical delivery after files, materials and tests are reviewable.
Design-to-process decisions
Translate flex construction into an assembly plan
A flexible circuit is not a rigid board that happens to bend. The released design must show where bending is allowed, how the circuit is supported during assembly and which dimensions or components control fit.
| Decision area | What to provide | What OrinewPCB reviews |
|---|---|---|
| Flex stack-up and materials | Layer construction, copper, coverlay, adhesive, stiffeners and finished thickness | Fabrication compatibility, thermal exposure and handling |
| Bend and transition zones | Bend radius, dynamic or static use, keep-outs and installation state | Risk of copper, coverlay or component stress |
| Panel or carrier | Array, tooling holes, rails and support method | Print, placement, reflow and depanel handling |
| Component restrictions | Package height, connector load, polarity and temperature limits | Sequence, support, profile and inspection access |
| Test and final form | Fixture, contact points, firmware, flexed or flat test state | Acceptance evidence and safe handling |
Keep components, vias and abrupt copper transitions away from defined bend regions unless the design has been specifically engineered and qualified for them. A separate rigid-flex construction should be reviewed on its own page rather than treated as a synonym for flexible PCB assembly.
Share the released data set for a combined engineering and BOM review. The quotation can then state the fabrication, sourcing, assembly, inspection and test assumptions together.
Nine controlled quality gates
A one-stop workflow for the complete assembly
A specialized board still needs the same configuration discipline as any repeatable PCBA. The method below connects procurement, process setup and acceptance evidence; it is not a claim that every product receives identical equipment or every optional test.
- Data and revision review: Reconcile fabrication files, BOM, placement data, drawings, quantities and product variants before material release.
- Source and material identity: Confirm PCB material requirements and exact manufacturer part numbers; any alternate remains subject to the agreed approval rule.
- Incoming inspection: Check received bare boards and components against the released order and the condition required for production.
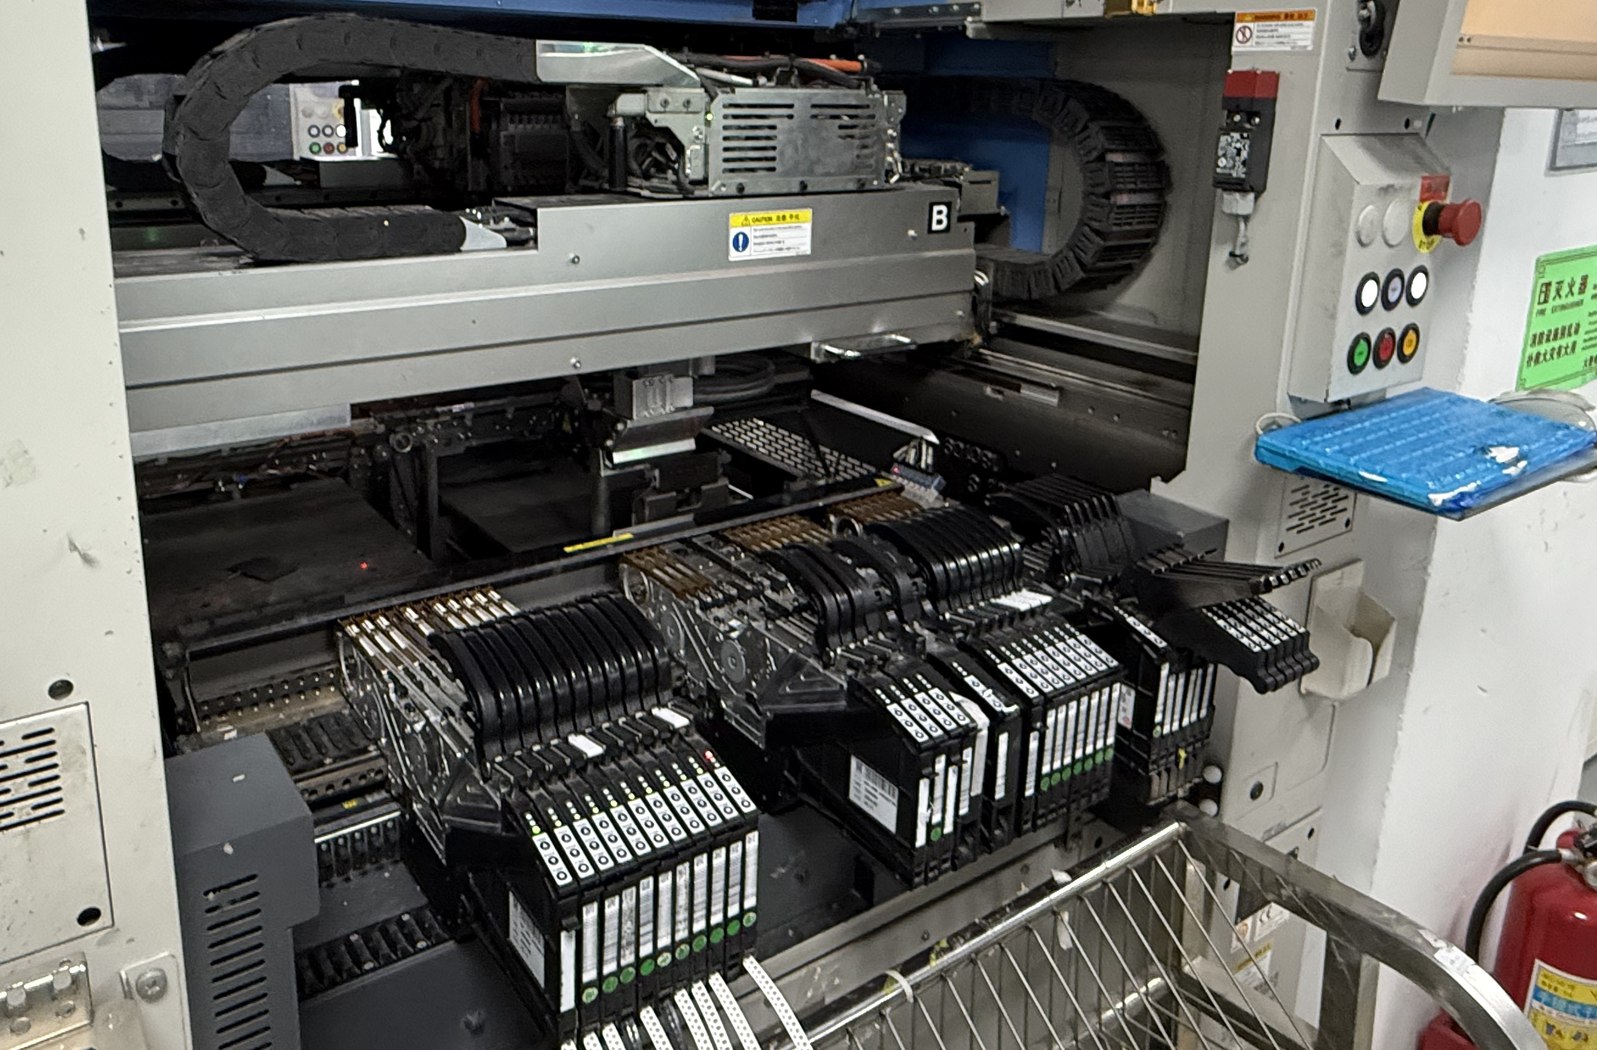
- Process setup and solder paste: Prepare stencil, tooling, support, feeders and solder-paste controls for the actual board construction.
- First-article verification: Verify polarity, orientation, fitted references and critical assembly attributes before the lot continues.
- AOI or visual inspection: Inspect visible soldering and placement attributes using the method appropriate to the board and package mix.
- X-ray where appropriate: Use X-ray when selected hidden joints or package structures require evidence that visible inspection cannot provide.
- Electrical or functional test: Apply the agreed test method, fixtures, firmware, limits and failure disposition for the product.
- Final quality and release: Reconcile quantity, records, approved deviations, packing and shipment release against the order.
Inspection scope is product-specific. AOI, X-ray, electrical testing and functional testing answer different questions. The applicable coverage depends on component packages, visibility, test access, fixtures, software and customer acceptance criteria.
Board-specific process control
Support the flex during printing, placement and inspection
A carrier or panel can keep the circuit flat enough for solder-paste printing and placement, but it must not trap the assembly, interfere with connectors or create uncontrolled stress at removal. Tooling and fiducials should support repeatable registration.
The thermal profile must reflect the flex materials, copper distribution, component mass and solder system. Excess handling after reflow can damage hot or unsupported circuits, so movement, cooling and depanel steps should be defined before the build.
Inspection also needs a planned presentation state. Visible joints can be checked by visual or AOI methods; hidden joints require a different evidence path. Functional testing should state whether the circuit is flat, installed or flexed during the test.
Original components · Coordinated supply
Component sourcing, cost and delivery are connected
Material price is only useful when the exact manufacturer part number, packaging, quantity and delivery window are correct for the released BOM. OrinewPCB checks manufacturer and distributor channels for genuine supply, available price breaks and practical lead time. We do not replace an approved component without the defined customer decision.
| Project input | How it supports cost | How it supports delivery |
|---|---|---|
| Exact manufacturer part numbers | Prevents quotes based on a different grade, package or lifecycle status. | Lets purchasing check real stock and authorized supply paths immediately. |
| Approved alternatives and authority | Creates a controlled comparison instead of an unreviewed substitution. | Reduces waiting when the preferred part is constrained. |
| Quantity by board variant | Allocates common material and setup cost to the correct models. | Supports a coordinated high-mix build sequence and material plan. |
| Firmware and test readiness | Shows programming, fixture and labor scope before the quote is confirmed. | Prevents assembled boards from waiting for an undefined acceptance method. |
For a wider responsibility matrix, review turnkey PCB assembly. For several models in practical quantities, the low-volume, high-mix PCB assembly page explains why variant control matters.
Build-ready information
What to send for an accurate PCBA review
- Gerber or ODB++, drill files, stack-up, board drawing and material requirements.
- BOM with exact MPNs, references, quantities, DNP lines and approved-alternate rules.
- Centroid or pick-and-place data, assembly drawings, polarity and mechanical notes.
- Quantity and revision for every board model or variant.
- Programming files, test instructions, fixtures, pass limits, records and target date.
Files should identify the same release. Mark preliminary data clearly and list unresolved decisions; a fast response is more reliable when engineering does not need to infer which version governs the build.
Related service detail is available in the flexible PCB manufacturing overview and one-stop PCB assembly pages.
From first build to repeat order
Keep the high-mix program traceable after the first shipment
The final production record should identify the actual PCB revision, installed manufacturer part numbers, approved alternates, programming version, inspection findings, rework and test limits. A repeat order should begin from that evidence and a newly reviewed release, not from an assumption that every file and component is unchanged.
For several product variants, use a configuration matrix that separates shared material from model-specific parts, DNP positions, firmware and test instructions. Common purchasing can support competitive component cost and supply planning, while separate traveler or lot records preserve the identity of each finished model. When one variant changes, state whether existing boards, components, stencil, fixtures or programs remain valid for the others.
Nonconformities also need a documented decision. Define who can approve a controlled deviation, alternate or rework, what evidence is required after correction and whether the disposition applies to one board, one lot or future releases. This prevents a fast answer during an urgent build from becoming an unintended permanent change.
Forecast information can help purchasing review allocation and common materials, but forecast demand should remain distinct from an authorized order. State likely quantities and timing separately from firm release quantities. For a new design, prototype PCB assembly can establish the build and test baseline before recurring low- or medium-volume production.
Frequently asked questions
Flexible PCB Assembly Services FAQ
These answers describe the manufacturing review boundary. The approved quotation, released product data and agreed acceptance plan remain the controlling documents for each order and variant.
What is flexible PCB assembly?
It is the controlled assembly of electronic components onto a flexible printed circuit, including support, soldering, inspection and the agreed electrical or functional test.
Can OrinewPCB manage components and flex fabrication together?
Yes. The reviewed one-stop scope can include flex fabrication, 100% new original components sourced by OrinewPCB, assembly and agreed testing.
How are bend areas handled during assembly?
The released design should identify bend areas and keep-outs. Carriers, panel support, handling and final test state are then planned around those constraints.
Is every flex assembly tested the same way?
No. Visible inspection, X-ray and electrical or functional tests provide different evidence. Coverage is defined from the component packages, access, fixture and product acceptance criteria.
Is flexible PCB assembly suitable for high-mix orders?
Yes, when every model has a controlled BOM, placement package and test definition. Shared materials can be planned while each variant remains separately traceable.
Send the flex stack-up, released fabrication and assembly data, BOM, quantities, bend requirements and test method. We will review the complete route before confirming price and schedule.
Send the BOM, board files, quantities and target date for a project-specific quote.
US keyword data used for this update: flex circuit assembly (70 monthly searches; keyword difficulty 0).