
OrCAD PCB Design: Move from Schematic Capture to Layout and Release
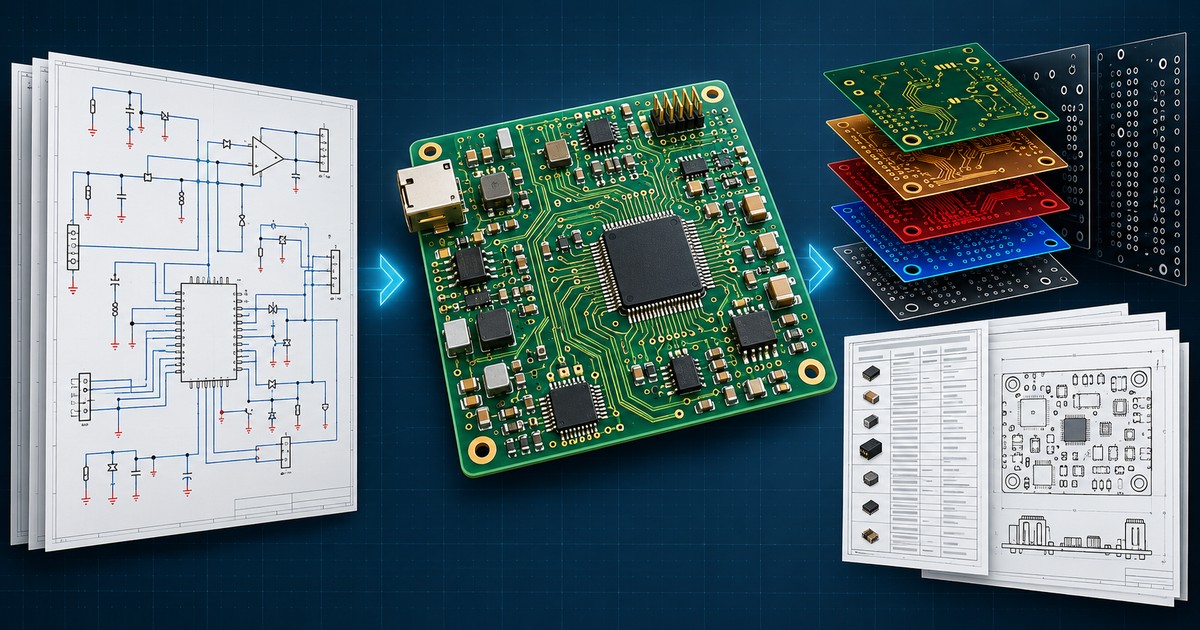
Table of Conent
Table of Conent
OrCAD PCB Design: Move from Schematic Capture to Layout and Release
An OrCAD PCB design is ready for manufacturing only when the schematic, component data, constraints, layout database, and release package describe the same controlled product. The reliable workflow is not simply “draw the schematic, route the board, export Gerbers.” It is a sequence of verifiable handoffs: validate the schematic, qualify symbols and footprints, transfer connectivity and constraints, establish the stackup and fabrication rules, place and route against those rules, run electrical and manufacturing checks, and release a versioned package that fabrication and assembly teams can interpret without guessing.
This guide focuses on the handoff decisions that reduce avoidable PCB fabrication and assembly questions. Menu names vary across OrCAD and OrCAD X versions, so treat the workflow as a release-control framework and confirm exact commands in the documentation for your installed tool version.
Define the release contract before schematic capture
The fastest design flow starts by defining what “released” means. Before engineers create pages and nets, establish the board revision scheme, controlled library source, intended layer count, key electrical interfaces, mechanical envelope, manufacturing outputs, and the people authorized to approve changes. This prevents the final export from becoming the first moment when missing files or ownership gaps are discovered.
A practical release contract identifies the authoritative schematic and PCB databases, the BOM source, the approved component and footprint libraries, the fabrication drawing, assembly drawings, placement data, drill and copper outputs, stackup notes, impedance requirements, and test requirements. It should also define how variants, do-not-populate parts, alternates, and engineering changes are represented.
Cadence describes OrCAD Capture as supporting hierarchical design, reuse, variants, part information, and integration with PCB design products. Those capabilities are useful only when the project team agrees which data source controls each downstream artifact. A schematic annotation, BOM export, and assembly drawing that disagree on a reference designator create a production ambiguity even if each file opens correctly.
Build a schematic that can survive the layout handoff
A layout-ready schematic has verified connectivity, stable reference designators, qualified library parts, explicit power intent, and resolved rule-check findings. Run the schematic electrical rule checks, then review warnings rather than clearing them in bulk. Unconnected pins, hidden power pins, conflicting output drivers, swapped units, and inconsistent net aliases can all produce a valid-looking drawing but an incorrect connectivity transfer.
Library validation deserves its own gate. Confirm the logical pin numbers match the package pad numbers, the pin-one convention is unambiguous, polarity and orientation marks agree, the land pattern matches the selected package option, and the 3D or mechanical representation does not hide a height or courtyard conflict. The related PCB library verification workflow explains why symbol, footprint, and part-number control should be completed before routing begins.
For multi-channel or hierarchical designs, review how repeated blocks, off-page connectors, and net aliases flatten into the physical database. Also lock the annotation direction before BOM and layout work branch into separate revisions. A late reference-designator reshuffle can invalidate placement instructions, inspection programs, test documentation, and procurement records.
Transfer connectivity and constraints as one controlled handoff
The schematic-to-layout transfer should move more than a netlist. It should preserve component identities, connectivity, classes, differential-pair definitions, critical-net intent, and any constraints created during capture. Cadence’s current guidance describes transferring schematic constraints into the PCB environment and then verifying them in Constraint Manager. The key manufacturing lesson is simple: never assume a successful import means every design rule arrived correctly.
After creating or updating the board database, compare component counts, net counts, unplaced parts, changed packages, and deleted or renamed nets. Review the update report and investigate unexpected differences. Then open the PCB-side constraint environment and confirm that physical, spacing, electrical, and manufacturing constraints are active where intended. If the team uses separate schematic and layout owners, record who reviewed this synchronization and which database revision was accepted.
Constraint sets should reflect actual engineering and supplier requirements, not generic defaults. Typical inputs include minimum conductor width and spacing, via structures, annular-ring expectations, copper-to-edge clearance, differential-pair geometry, length matching, component clearances, solder-mask rules, and test-point access. The recently published layer, rule, and library setup checklist applies across CAD platforms and helps expose these inputs before placement.
If a project is approaching layout release, share the schematic, preliminary BOM, stackup assumptions, and critical constraints for a combined fabrication and assembly review. That package gives manufacturing engineers enough context to flag library, sourcing, clearance, and process assumptions before the route is frozen.
Set up the board database before placement
A stable board setup turns mechanical and manufacturing requirements into the geometry that placement and routing must respect. Import or recreate the approved outline, cutouts, mounting features, connector locations, keepouts, height limits, and panel-interface assumptions. Define the cross-section with the intended signal and plane layers, dielectric relationships, copper weights, and controlled-impedance notes where applicable.
Do not select trace widths or via structures from habit. Coordinate them with current capacity, impedance targets, breakout density, aspect ratio, drilling capability, annular ring, and cost. When exact construction is supplier-dependent, state the electrical targets and allow the fabricator to propose a manufacturable stackup before the design is treated as final.
Placement begins with mechanical anchors and high-risk interfaces: connectors, switches, sensors, antennas, heat-producing parts, isolation zones, fine-pitch packages, and components constrained by enclosure access. Place support circuitry around the function it serves rather than filling empty space first. Check polarity, pin-one visibility, component orientation strategy, courtyard spacing, rework access, and inspection visibility while changes are still inexpensive.
Route with constraints active and review exceptions intentionally
Constraint-driven routing is valuable because violations are detected close to the decision that caused them. Cadence documents physical, spacing, electrical, manufacturing, rigid-flex, and 3D constraint categories, with real-time feedback available in current OrCAD X environments. A clean canvas is not enough, however; the team must confirm the relevant constraints are enabled, correctly scoped, and based on released requirements.
Route critical nets first when their topology, return path, impedance, skew, current, or noise sensitivity controls placement. Review layer transitions, reference-plane continuity, return-via strategy, neck-down regions, stubs, copper pours, thermal connections, and spacing near board edges or high-voltage areas. For ordinary nets, maintain a consistent routing style that simplifies review rather than optimizing only for completion speed.
Every waived violation should have an owner and rationale. A waiver can be legitimate—for example, a localized geometry approved by the fabricator—but an unexplained marker teaches the next reviewer nothing. Keep an exception record tied to the design revision and confirm that a later database update does not silently reintroduce the condition elsewhere.
Validate electrical intent and manufacturability separately
Final validation should distinguish connectivity and electrical constraints from fabrication, assembly, and testability checks. First confirm all intended nets are connected, prohibited shorts are absent, differential and timing constraints pass, plane assignments are correct, and unresolved DRCs have documented dispositions. Then perform a manufacturing-focused review of minimum features, mask and paste geometry, drill structures, copper-to-edge spacing, silkscreen, component clearances, polarity visibility, tooling access, and test-point access.
Cadence’s DesignTrue documentation separates checks for fabrication, assembly, and test, which is a useful way to organize the signoff even when a project does not license every automated check. Automated analysis should be supplemented by supplier rules and a visual review. The ERC, DRC, and release automation guide shows where scripts improve repeatability and where human review still matters.
Run a controlled comparison between schematic connectivity, PCB connectivity, BOM, and placement outputs. Confirm all populated references exist in both BOM and placement data, excluded references are intentional, package names are stable, and coordinates use the declared origin, side, rotation convention, and units. A technically correct layout can still fail the production handoff if its supporting files describe a different revision.
Generate a release package that can be independently checked
A manufacturing release should be reproducible from a known database revision and complete enough for an independent reviewer to identify what will be built. Cadence’s OrCAD X workflow includes manufacturing-output generation and version-controlled release content; regardless of tool version, the exported set should be treated as one immutable package rather than a folder assembled from several dates.
Typical fabrication deliverables include copper, solder-mask, silkscreen, paste or other required artwork; NC drill and route data; a fabrication drawing; stackup and material notes; controlled-impedance requirements; and a readme that identifies format, units, zero suppression where relevant, revision, and special instructions. Assembly deliverables commonly include the BOM, centroid or pick-and-place data, assembly drawings for each side, polarity and special-process notes, approved alternates, test requirements, and programming files when applicable.
Choose output formats intentionally. The PCB manufacturing data format comparison explains the tradeoffs among Gerber, ODB++, IPC-2581, drill data, and drawings. Intelligent formats can carry richer relationships, but a supplier still needs a clear revision, readable documentation, and agreement on which file is authoritative when formats overlap.
Use a release checklist before sending the package
A concise release checklist prevents the same high-cost omissions from recurring:
- Freeze the approved schematic, PCB database, libraries, and revision identifiers.
- Confirm schematic and PCB connectivity are synchronized with no unexplained changes.
- Verify stackup, outline, holes, cutouts, keepouts, layer use, and impedance notes.
- Resolve or formally waive electrical, physical, fabrication, assembly, and test findings.
- Cross-check reference designators across the PCB, BOM, placement data, and drawings.
- Review generated copper and drill outputs in an independent viewer.
- Confirm file units, origin, rotation convention, board side, revision, and naming.
- Package fabrication, sourcing, assembly, programming, and test requirements together.
- Archive the release manifest and checksums so later changes are detectable.
The same package can support a broader PCB assembly manufacturing review when fabrication, component sourcing, SMT or through-hole assembly, and testing need to be coordinated under one build plan.
Conclusion
A dependable OrCAD PCB design workflow is a chain of controlled agreements. The schematic defines connectivity and design intent; verified libraries connect that intent to real packages; constraints carry requirements into placement and routing; separate electrical and manufacturing checks test the result; and a versioned release package makes the build reproducible. Skipping any handoff merely postpones the question until it is more expensive to answer.
Before production, review the released artifacts as a manufacturer would: can another team identify the exact revision, source every populated part, fabricate the intended stackup, orient every component, program and test the assembly, and trace every approved exception? If the answer is not yet clear, provide the released Gerber or intelligent manufacturing data, BOM, placement file, drawings, build quantity, and test requirements for engineering review so the manufacturing scope and unresolved assumptions can be checked together.
Official OrCAD workflow references
Latest Blog
Contact Info
Phone: +86-755-82882936
Email: [email protected]
WhatsApp: +86-13570802455
Wechat: +86-13570802455
Address: 2nd floor,D Bldg.,Electric Link Technology Bldg.,Gongming,Guangming New Dist.,518106 Shenzhen, China