
EVT Build Handoff: Assign Owners for Files, Parts and Test Readiness
Table of Conent
Table of Conent
An EVT build handoff should convert an engineering design into one controlled, buildable, and testable release. It is not a file dump and it is not a meeting where every open question is assigned to the contract manufacturer. The handoff is complete when each deliverable has a named owner, revision, due date, acceptance condition, and documented disposition.
This guide explains how to prepare an engineering validation test build for PCB assembly. It focuses on the interfaces that most often create schedule slips: design files, component decisions, fabrication assumptions, assembly instructions, programming, fixtures, and test evidence. If you are preparing an EVT lot, AssyPCB can review the controlled package and quote the PCB assembly build after you provide the released files, quantities, schedule, and required inspection or test scope.
What EVT build readiness means
Companies use EVT, DVT, and PVT differently, so the letters alone do not define the required evidence. For this article, an EVT build is an engineering build used to evaluate whether the integrated hardware behaves as intended and whether the team understands the design and manufacturing risks well enough to advance. The build may expose design defects, component constraints, process limits, test gaps, or mechanical integration problems. That is useful, provided the configuration and observations are traceable.
Build readiness means that the team can answer five questions before material or line time is committed:
- Which exact hardware, firmware, and mechanical configuration will be built?
- Are the data package and component decisions internally consistent?
- Can the supplier fabricate, assemble, program, inspect, and test the units as requested?
- Who owns each open issue, and what decision date protects the build?
- What evidence will determine whether the build met its engineering objectives?
These questions reflect broader configuration-management and verification principles. NIST defines configuration management as maintaining consistency between a product’s attributes, requirements, design information, and operational information. NASA systems-engineering guidance similarly emphasizes controlled test articles, support equipment, responsibilities, and verification methods. FDA design-transfer guidance, while applicable in a regulated context, makes a broadly useful point: production specifications must translate design knowledge into instructions that can repeatedly produce the intended result. An EVT handoff should apply those principles in proportion to the product’s risk and maturity.
Start with one configuration baseline
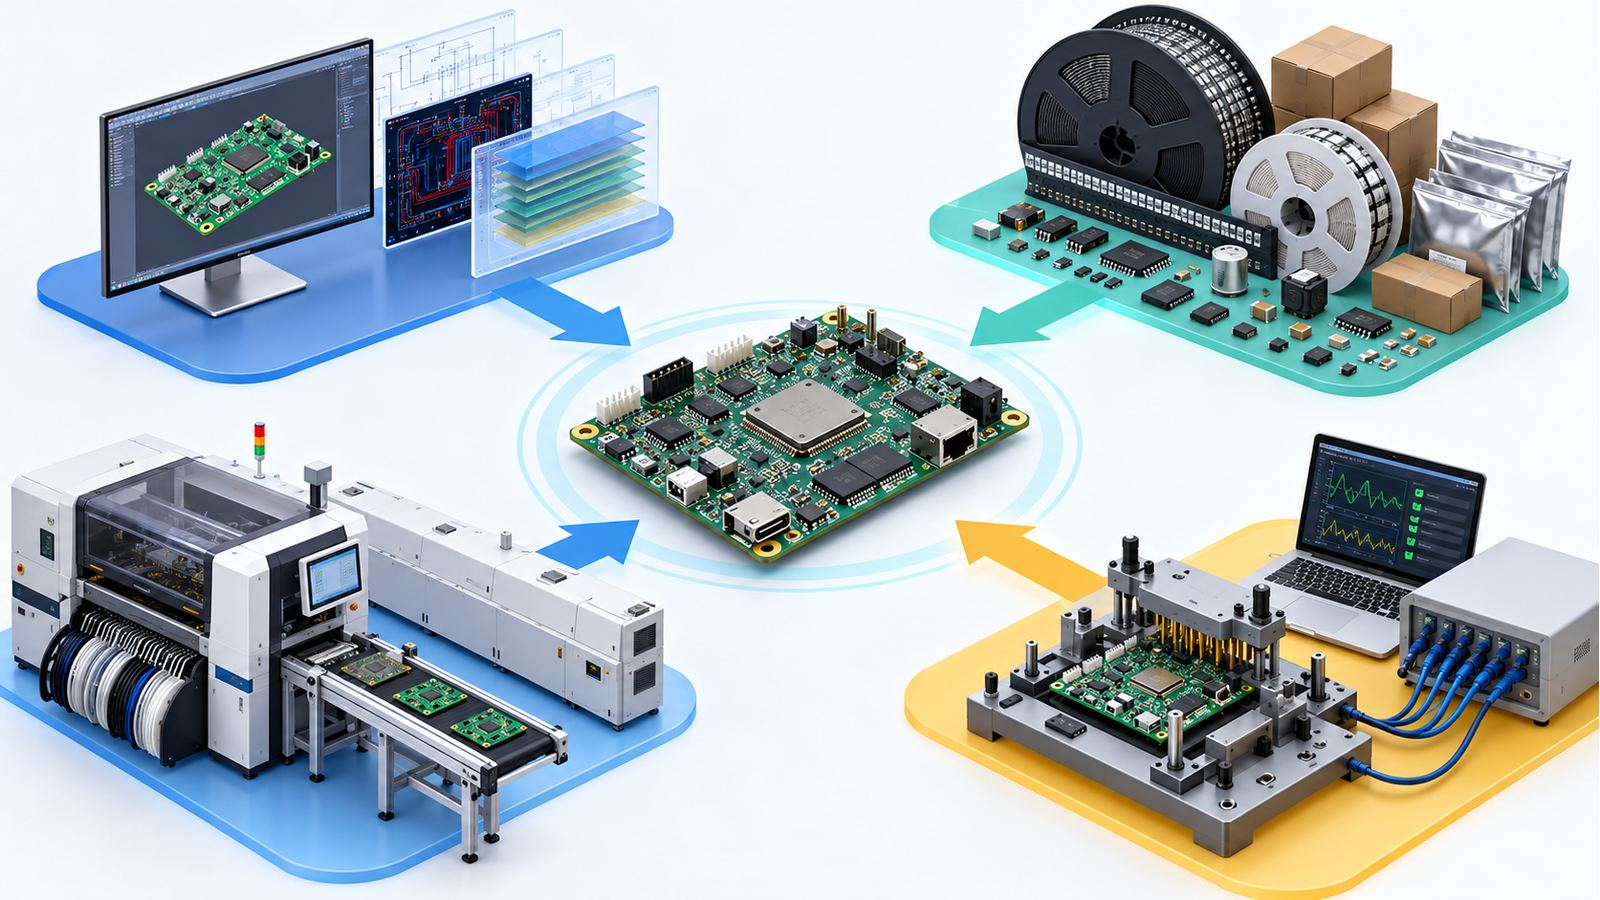
The first readiness decision is not whether the Gerbers are finished. It is whether all released artifacts describe the same product revision. Create a configuration record that names the schematic revision, PCB layout revision, fabrication output package, fabrication drawing, stackup, impedance requirements, BOM revision, approved alternates, centroid file, assembly drawing, mechanical model, firmware image, programming procedure, test specification, fixture revision, and enclosure or harness revision.
Use stable identifiers rather than filenames such as “final,” “latest,” or “use_this.” A practical release record includes the document number, revision, release date, owner, checksum or controlled repository location, and approval state. If a file is intentionally preliminary, mark it as preliminary and document the decision it is waiting on. Do not let an unreleased file silently become the manufacturing master because it was attached to the newest email.
Perform a cross-file reconciliation before handoff. The BOM must match the schematic and assembly variant. Reference designators must agree across BOM, centroid data, assembly drawing, and programming or test documents. Board outline, hole locations, cutouts, connectors, height limits, keepouts, and polarity indicators must agree with the mechanical model and drawing. The PCB assembly drawing checklist is a useful starting point for this review.
Assign owners to deliverables, not departments
“Engineering owns it” is not an assignment. Name one accountable person for every readiness item, even when several specialists contribute. The owner is responsible for obtaining the required input, recording the decision, updating the controlled artifact, and communicating the disposition.
| Readiness area | Typical accountable owner | Evidence at release |
|---|---|---|
| Electrical design and PCB data | Hardware lead | Approved schematic, layout outputs, drawings, and change summary |
| Mechanical interfaces | Mechanical lead | Board model, enclosure interfaces, connector constraints, and fit criteria |
| BOM and alternates | Hardware or component engineer | Controlled BOM, exact MPNs, approved alternates, and decision records |
| Procurement status | Buyer or supply-chain owner | Source, quantity, date code or traceability needs, and shortage disposition |
| Assembly process | Manufacturing engineer | Stencil, profile, special handling, workmanship, and inspection requirements |
| Firmware and programming | Firmware lead | Released binary, checksum, configuration, procedure, and verification step |
| Test readiness | Test lead | Fixture, equipment, scripts, limits, sample plan, and data-record format |
| Build authorization | Project or engineering manager | Accepted open-item list, quantity, schedule, budget, and release approval |
The supplier also needs named contacts for technical questions, commercial decisions, and urgent deviation approvals. Set response-time expectations before the line is scheduled. A two-day engineering delay can consume the production slot even when assembly itself takes only hours.
Use a readiness matrix with measurable exit criteria
A useful handoff matrix is more than a checklist of files received. For each item, include the owner, required revision, due date, status, blocking condition, evidence link, and reviewer. Define statuses precisely. “In progress” should identify the missing decision. “Complete” should mean the current artifact has been reviewed and placed under control.
Separate blockers from accepted risks. A blocker prevents the requested build from producing meaningful hardware, such as a missing drill file, unresolved footprint mismatch, unavailable sole-source component, or nonexistent programming method. An accepted risk allows the build to proceed with a documented consequence, owner, and containment plan. Examples include using a nonpreferred but electrically approved component on a small subset or running a manual test while the automated fixture is completed.
Establish the freeze date and the last responsible decision date for each long-lead item. A design can remain open while components are ordered only when the team understands which changes would invalidate the purchase or require rework. Record those boundaries explicitly.
Release a fabrication package that can be interpreted once
The PCB fabrication package should include the manufacturing outputs and the engineering requirements needed to interpret them. Depending on the design, this can include Gerber or ODB++/IPC-2581 data, NC drill and route data, a fabrication drawing, board outline definition, controlled stackup, finished copper thickness, material requirements, impedance targets and coupons, surface finish, solder-mask and legend requirements, via structures, tolerances, panel constraints, serialization, and electrical-test requirements.
Do not rely on a purchase-order note to override contradictory drawing or data content. Resolve conflicts before release and define an order of precedence for unavoidable ambiguity. Confirm that the board revision visible on the drawing and artwork matches the release record. If the supplier proposes a stackup or material substitution, identify who may approve it and what electrical or reliability review is required.
EVT quantities are small, but small quantity does not justify losing traceability. State whether fabrication coupons, impedance reports, electrical-test reports, material certificates, microsections, or lot identification are needed. Request only evidence that serves a defined engineering objective.
Make the BOM an engineering-controlled input
A buildable BOM needs manufacturer names, exact manufacturer part numbers, quantities per assembly, reference designators, descriptions, package or value data, population status, and approved alternates where applicable. Distributor SKUs can support purchasing, but they should not replace the manufacturer identity. Generic descriptions such as “10 uF capacitor” are insufficient when voltage rating, dielectric, case size, tolerance, bias behavior, or qualification affects function.
Resolve lifecycle and availability issues before the kit reaches the line. For constrained parts, record whether the team will wait, redesign, approve an alternate, use customer-supplied inventory, or build a reduced quantity. The BOM alternate approval workflow explains how to verify the exact replacement rather than approving a family description.
Define traceability and handling requirements for sensitive items. These may include lot or date-code control, authorized-source restrictions, moisture-sensitivity handling, bake limits, electrostatic-discharge precautions, programming status, calibration data, or unique serialization. Clarify whether partial reels, trays, loose parts, and consigned materials are acceptable and how remaining material should be returned or retained.
Translate design intent into assembly instructions
The assembler should not have to infer critical intent from the schematic. Release an assembly drawing or equivalent document that identifies the populated variant, DNP references, polarity, orientation, hardware, connector position, wire or cable installation, labeling, conformal coating or masking, thermal-interface materials, adhesive, staking, torque, and cleanliness requirements.
Call out features that need special process planning: bottom-terminated components, large thermal pads, fine-pitch packages, press-fit hardware, odd-form parts, heavy copper, mixed thermal mass, through-hole connectors, hand-soldered wires, selective solder, multiple reflow cycles, or temperature-sensitive components. Indicate inspection methods when they are important to the engineering objective, such as X-ray for hidden joints or dimensional verification for a mating connector.
Discuss stencil and reflow assumptions before the build. Aperture design, step stencils, paste type, carrier or pallet needs, and profile development can affect first-pass yield and the relevance of EVT observations. The PCB assembly process guide shows how material control, printing, placement, reflow, inspection, and test connect.
Prepare firmware and programming as controlled manufacturing inputs
Firmware readiness requires more than a binary file. Identify the target hardware revision, bootloader dependencies, configuration bytes, security or key-handling constraints, programmer and adapter, fixture connection, power sequence, programming voltage, expected duration, checksum, and pass/fail verification. Define whether devices arrive preprogrammed, are programmed before placement, are programmed in circuit, or are loaded after final assembly.
Keep engineering debug builds separate from the image intended for the EVT lot. If multiple images or configurations are required, map each one to serial numbers or build variants. Record the programmed version on the unit or in the traceability database. Include a recovery procedure for interrupted or failed programming and define who can authorize a reflash.
Run the procedure on representative hardware before line release. Confirm connector access, cable orientation, driver installation, license availability, script paths, and communication settings. A procedure that worked only on the firmware developer’s bench is not yet a manufacturing instruction.
Make test readiness part of the build plan
Define what the EVT build must learn. Objectives may include power-rail validation, current consumption, interface operation, sensor accuracy, thermal behavior, programming yield, bring-up sequence, manufacturing defect detection, fixture access, or mechanical fit. Each objective should have a method, equipment, unit configuration, precondition, acceptance criterion, data record, and owner.
Distinguish manufacturing inspection from engineering validation. AOI, X-ray, electrical test, and functional test can detect different defect classes, but none automatically proves the product meets all design requirements. Conversely, an engineering bench test may demonstrate performance while missing repeated assembly defects. The PCBA testing guide provides context for combining these methods.
Verify the fixture and script before production boards arrive. Confirm probe access, connector durability, board support, clamping force, safety interlocks, power limits, instrument calibration, software version, log naming, database access, and golden-unit behavior. Use known-pass and, where practical, known-fail conditions to verify that limits and channels are not reversed or stale.
Define the data package expected after the build. Useful records can include unit identity, board and firmware revision, component variant, operator, equipment ID, fixture and script revision, raw measurements, failures, retest history, rework, deviations, and final disposition. Avoid collecting data that no one will review, but do not discard raw evidence needed to diagnose yield or performance.
Plan first-article review and stop points
Do not release the entire EVT quantity through every process step before reviewing the first result. Define stop points based on risk. Common examples include bare-board inspection, solder-paste print review, first-off placement inspection, post-reflow X-ray, initial power-up, programming, and mechanical fit.
Specify who must be available at each stop point and what evidence permits continuation. A first-article review should compare the unit to the controlled package, not to memory. Photograph relevant features, record deviations, and preserve measurements. If a correction changes the assembly process, fixture, firmware, or design data, control that change before restarting.
Clarify whether reworked EVT units can support later tests. Rework may be appropriate for diagnosis or continued learning, but it can alter thermal, electrical, mechanical, or reliability behavior. Mark reworked units and record the procedure so the team does not mistake them for untouched production-intent samples.
Control open issues without hiding them
A handoff can proceed with open items when the team understands their boundaries. Maintain one open-item register with the issue, impact, owner, due date, decision authority, affected files or units, and containment action. Link each issue to the build record and update it as evidence arrives.
Avoid three failure modes. First, do not bury technical questions in separate email chains. Second, do not allow a purchasing substitution to become an engineering decision by default. Third, do not treat a supplier deviation as approval for future builds. Each temporary disposition should identify the specific lot or serial numbers it covers.
When an issue changes the baseline, revise the affected artifacts and communicate the new release as a complete delta. A verbal instruction during a video call is not a controlled change. Preserve superseded files so the as-built configuration remains reconstructable.
A practical EVT handoff sequence
- Define build objectives. State what the lot must prove or teach and how results will be used.
- Freeze the candidate baseline. Record all hardware, firmware, mechanical, and test revisions.
- Reconcile the package. Check BOM, centroid, drawings, variants, mechanical interfaces, and reference designators.
- Review material risk. Confirm exact parts, sources, quantities, alternates, handling, and shortage decisions.
- Review fabrication and assembly risk. Resolve stackup, stencil, profile, tooling, inspection, and special-process questions.
- Prove programming and test access. Run procedures, fixtures, scripts, and data capture on representative hardware.
- Assign every open item. Set owners, decision dates, containment, and escalation paths.
- Authorize the build. Approve quantity, schedule, budget, accepted risks, stop points, and communication rules.
- Review first articles. Compare the actual unit with the controlled package before releasing the balance.
- Close with as-built evidence. Record serial numbers, deviations, rework, test results, unused material, and recommended design changes.
Common EVT handoff mistakes
- Sending Gerbers before BOM, drawing, and variant decisions are aligned.
- Using “latest” files without revision identifiers or release approval.
- Assigning actions to a department instead of one accountable person.
- Ordering substitute components before engineering reviews the exact MPN.
- Providing firmware without a checksum, hardware mapping, or verification step.
- Scheduling the line before fixtures, scripts, equipment, and limits are ready.
- Running the full quantity before first-article inspection and power-up.
- Mixing reworked, prototype, and production-intent units in the same evidence set.
- Accepting deviations without identifying the units and future-build applicability.
- Closing the build without an as-built configuration and failure record.
Frequently asked questions
How complete must the design be before an EVT build?
The design does not need to be proven, because learning is the purpose of EVT, but the build configuration must be defined. Intentional experiments and accepted risks should be explicit. Uncontrolled contradictions between files are not useful experiments.
Who owns EVT readiness?
One project or engineering lead should own the overall release, while named specialists own their deliverables. The contract manufacturer owns execution within the agreed process and should surface manufacturability concerns, but product requirements and engineering acceptance remain with the designated customer authorities.
Can component procurement start before design freeze?
Yes, when the team records which purchases are safe, what design changes would invalidate them, and who accepts the commercial risk. Long-lead procurement should not silently lock an unapproved design choice.
What should be reviewed at the first-article stop?
Review identity and revision, workmanship, polarity and orientation, critical dimensions, hidden-joint evidence where required, shorts or opens, current-limited power-up, programming, essential functions, and any feature tied to a known risk.
What should the supplier return after the build?
Request the as-built configuration, unit identities, material and lot information required by the plan, inspection and test records, deviations, rework history, yield summary, failure evidence, remaining material status, and recommendations that affect the next revision.
Turn the handoff into a controlled engineering experiment
A strong EVT build does not depend on perfect information. It depends on explicit ownership, consistent files, bounded risks, ready materials, defined processes, proven programming and test methods, and traceable results. Build the readiness matrix early, keep one configuration baseline, and use first-article stop points to protect both hardware and schedule.
For an upcoming engineering build, send the fabrication package, controlled BOM, assembly data, firmware and programming method, quantities, schedule, special-process requirements, and test objectives. AssyPCB can review the EVT handoff and prepare a PCBA quotation before components or production capacity are committed.
Latest Blog
Contact Info
Phone: +86-755-82882936
Email: [email protected]
WhatsApp: +86-13570802455
Wechat: +86-13570802455
Address: 2nd floor,D Bldg.,Electric Link Technology Bldg.,Gongming,Guangming New Dist.,518106 Shenzhen, China