
Ongoing Reliability Testing: Detect Production Changes After Qualification
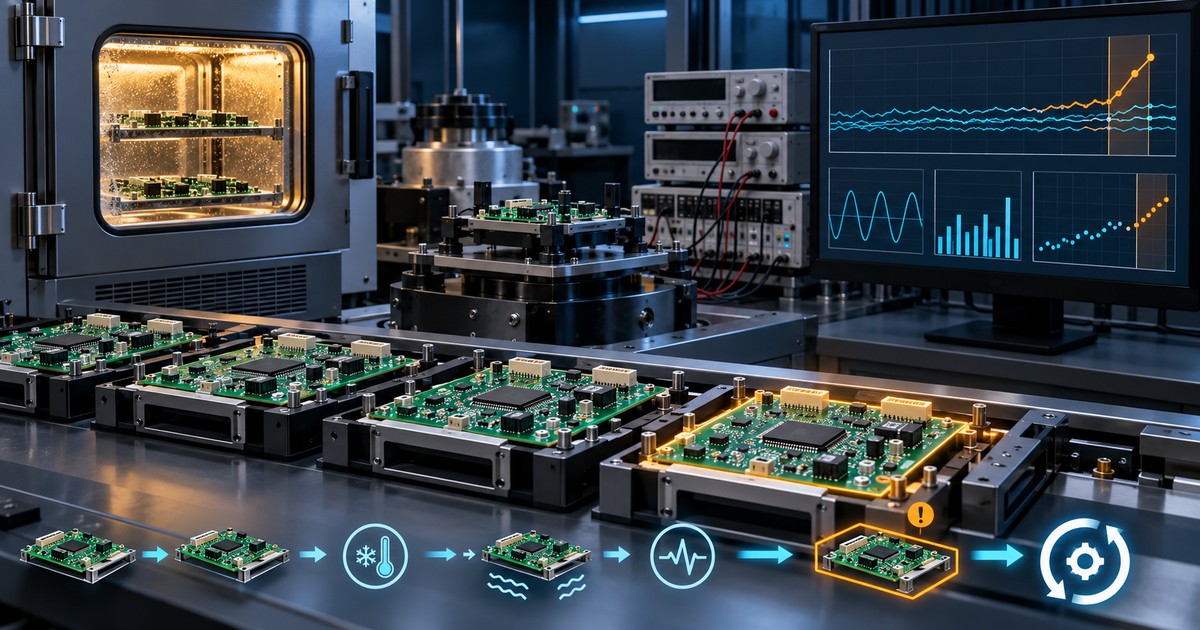
Table of Conent
Table of Conent
Ongoing Reliability Testing: Detect Production Changes After Qualification
Ongoing reliability testing (ORT) is a planned program that periodically samples current production and applies selected stresses or extended functional tests to detect changes that ordinary acceptance testing may miss. ORT does not requalify every lot, and it is not a substitute for process controls, inspection, or end-of-line functional test. Its value is trend detection after qualification: identifying shifts in materials, suppliers, tooling, assembly processes, workmanship, or test systems before field failures become the first warning.
An effective ORT program starts with product risks and qualification evidence, then defines representative samples, stress profiles, powered monitoring, acceptance criteria, trend rules, and a closed-loop response. The plan must fit the product’s use environment and change history; copying a generic temperature-cycle schedule can consume samples without testing the failure mechanisms that matter.
Separate qualification, production acceptance, screening, and ORT
These activities answer different questions. Qualification asks whether a design and process can meet defined requirements. Production acceptance verifies that a particular unit or lot meets release criteria. Screening applies stress to remove susceptible units, often at much higher coverage. ORT samples ongoing production to determine whether the qualified design and process remain stable over time.
The distinction controls how results are interpreted. A single ORT failure is not automatically proof that an entire shipped population is defective, but it is evidence that must be investigated against the predefined escalation plan. Likewise, passing sampled ORT does not prove that every unit will survive every service condition. Sampling, stress severity, duration, failure detection, and the relationship between the sample and production population all limit the claim.
MIL-PRF-19500 describes an ongoing reliability program as continuous sampling and testing tied to manufacturing processes, failure analysis, and improvement. That component-focused military specification should not be imposed on an unrelated commercial PCBA, but its closed-loop principle is broadly useful: the program should connect observed failures to process knowledge and corrective action rather than merely accumulate chamber hours.
Build the ORT plan from failure mechanisms
The test matrix should target credible latent weaknesses in the assembly. Begin with the product risk analysis, qualification results, field history, supplier changes, manufacturing process flow, and known design margins. Map each risk to a stress, monitored response, failure criterion, and evidence record. The related PCB test planning framework shows how to keep requirements, methods, limits, coverage, and records connected.
Temperature cycling may reveal solder-joint fatigue, plated-through-hole weakness, connector intermittency, or package-to-board coefficient-of-expansion interactions. Damp heat or biased humidity may expose contamination, coating gaps, leakage, corrosion, or electrochemical migration risks. Vibration can reveal connector, fastener, lead, and solder-joint weaknesses. Powered cycling and load profiles can stress regulators, power paths, motors, relays, heaters, LEDs, or communications interfaces. The chosen profile should reproduce a meaningful combination of electrical and environmental stress, not simply the harshest available condition.
Use applicable product requirements and controlled test methods. IPC publishes PCB environmental methods including thermal cycling, moisture and insulation resistance, vibration, and related evaluations. IEC 60068-2 organizes environmental test methods for electrotechnical products. IPC-9701 addresses thermal-cycling characterization of surface-mount attachments. These documents help define repeatable methods, but the product team still has to set the appropriate sample, severity, duration, monitoring, and acceptance criteria.
Choose samples that represent production changes
ORT sampling should provide traceability across time and known sources of variation. Record serial number, product revision, PCBA revision, manufacturing date, lot, line, shift when relevant, PCB supplier and lot, critical component lots, software or firmware version, rework history, and the configuration used during test. Without this genealogy, a trend signal cannot be linked reliably to a material or process change.
Sampling frequency can be based on time, production quantity, lots, or risk-triggered events. Stable, high-volume production may support periodic samples, while a supplier transition, new factory line, process transfer, component redesign, solder-paste change, or major engineering change may justify temporarily increased coverage. Risk and customer requirements should drive the rule; there is no universal sample size or interval that is correct for every assembly.
Retain a consistent baseline configuration where possible. If the product has multiple variants, decide whether they share the same root technology and stress response or need separate monitoring. A low-cost variant should not be treated as representative of a high-power or high-density variant when the critical failure mechanisms differ.
If the program is being established for a production build, share the released Gerber data, BOM, placement files, critical operating loads, qualification summary, and proposed ORT profile for manufacturing and test review. That evidence allows fabrication, sourcing, assembly, and test assumptions to be evaluated together before the sampling plan is frozen.
Monitor the product during stress, not only afterward
Powered monitoring improves fault detection because many reliability problems are intermittent. A board can pass a room-temperature functional check after the chamber has stopped while still losing communication, resetting, drifting, or opening briefly during temperature transitions or vibration. Instrument the functions that represent real failure: supply rails, current, communication error counts, sensor accuracy, timing, output load behavior, contact resistance, continuity, or application-specific performance.
Define data-acquisition rate, fixture channels, synchronization, calibration, software revision, allowable dropouts, alarm rules, and raw-data retention before testing. Include known-good control hardware or check standards when measurement drift could mimic product change. NIST guidance on measurement-process control emphasizes monitoring check standards over time to identify changes in bias and variability; the same discipline helps separate test-system drift from product drift.
Fixtures are part of the measurement system. Connector wear, cable resistance, relay aging, thermal gradients, condensation, vibration-fixture resonance, and software changes can create false failures or hide real ones. Schedule fixture inspection and verification, track channel-specific anomalies, and keep calibration and maintenance records with the test result.
Set acceptance criteria before results are visible
ORT criteria should include both unit-level failures and program-level trend rules. Unit criteria may cover functional loss, parametric drift, intermittent events, visual damage, insulation resistance, continuity, or performance outside a stated limit. Program criteria should define when a failure triggers containment, additional sampling, failure analysis, corrective action, or review of previously produced material.
Avoid changing limits after a concerning result unless the requirement was genuinely wrong and the change is formally approved. Record pretest, in-test, and post-test values so drift can be distinguished from abrupt failure. For destructive or life-consuming tests, state whether samples may return to production; typically they should remain controlled test articles unless an approved requirement explicitly permits otherwise.
Use trend charts carefully. Control limits describe historical process behavior, not product specification limits, and they should not be selected to guarantee a passing chart. NIST notes that Shewhart charts are intuitive for larger changes, while EWMA methods can be more sensitive to smaller sustained shifts. The method should match the data distribution, sample cadence, and decision risk. Sparse ORT failures may require attribute methods and engineering review rather than a continuous-variable chart.
Investigate failures with a closed-loop response
The response plan is what converts ORT from a laboratory activity into production protection. When a unit fails, preserve the evidence and test context, confirm the failure, rule out fixture or software artifacts, document the failure signature, and initiate analysis appropriate to the risk. Do not repeatedly retest until a unit passes and then erase the first result.
Containment scope should be based on traceability and the suspected mechanism. Review affected lots, dates, suppliers, process records, inspection data, repair logs, and field returns. If destructive analysis is needed, control the sequence so electrical evidence is not lost before cross-sectioning or component removal. Corrective action should address the verified cause, and effectiveness should be demonstrated through production evidence and, when appropriate, targeted repeat testing.
Engineering changes also require deliberate regression decisions. The DVT change-impact review method helps map a design, material, firmware, or process revision to affected requirements and tests. ORT can confirm continuing stability after the change, but it should not replace the qualification work needed when the change creates a new failure mechanism or invalidates earlier evidence.
Connect ORT to factory and field data
ORT is strongest when it is reviewed beside process and product evidence. Useful companion indicators include first-pass yield, defect paretos, AOI and X-ray findings, rework causes, in-circuit and functional-test distributions, supplier deviations, calibration events, field returns, and customer complaints. Correlation does not prove cause, but aligned changes can narrow the investigation and reveal whether the ORT sample is representative.
The control-board reliability test example illustrates how operating loads and realistic fault states can be incorporated into a product-specific plan. In production, the ORT owner should periodically review whether the stress profile still represents the product configuration and use environment. A program can become obsolete when components, PCB construction, coating, enclosure, firmware, or customer duty cycle changes.
Keep a controlled record for every sample: genealogy, test procedure revision, chamber and fixture IDs, calibration status, setup photographs where useful, software version, raw data, anomalies, failure analysis, disposition, and corrective-action linkage. A summarized pass result without raw evidence is difficult to audit or compare after the team, equipment, or supplier changes.
Use a practical ORT release checklist
Before launching or revising the program, confirm the following:
- The program objective and covered product revisions are explicit.
- Qualification, acceptance test, screening, and ORT roles are separated.
- Failure mechanisms link to justified stresses and monitored functions.
- Sample source, frequency, genealogy, and variant coverage are controlled.
- Stress levels, durations, transitions, operating loads, and fixtures are documented.
- Measurement channels, calibration, check standards, and data retention are defined.
- Unit acceptance limits and trend/escalation rules are approved before testing.
- Failure confirmation, containment, analysis, corrective action, and effectiveness checks have owners.
- Change control specifies when the plan must be reviewed or qualification repeated.
For programs that require coordinated fabrication, component sourcing, assembly, functional fixtures, and environmental testing, the PCB assembly service workflow provides the commercial path for aligning the build and verification scope.
Conclusion
Ongoing reliability testing is a surveillance system for a qualified product and process. It works when representative production samples are stressed against known risks, critical functions are monitored during the stress, results are trended with measurement-system controls, and every significant signal leads to a defined investigation and response. ORT fails when it becomes a ceremonial chamber cycle with weak genealogy, unclear limits, or no connection to corrective action.
Start with the failure mechanisms that could change after qualification, then build the smallest test matrix that can detect those changes with credible evidence. When a new production program needs that plan integrated with the actual build, provide the manufacturing package, expected use conditions, qualification evidence, sample cadence, and functional-test requirements for a combined scope review so unresolved coverage and traceability gaps can be addressed before routine testing begins.
Primary references
Latest Blog
Contact Info
Phone: +86-755-82882936
Email: [email protected]
WhatsApp: +86-13570802455
Wechat: +86-13570802455
Address: 2nd floor,D Bldg.,Electric Link Technology Bldg.,Gongming,Guangming New Dist.,518106 Shenzhen, China